

Industrial Chiller
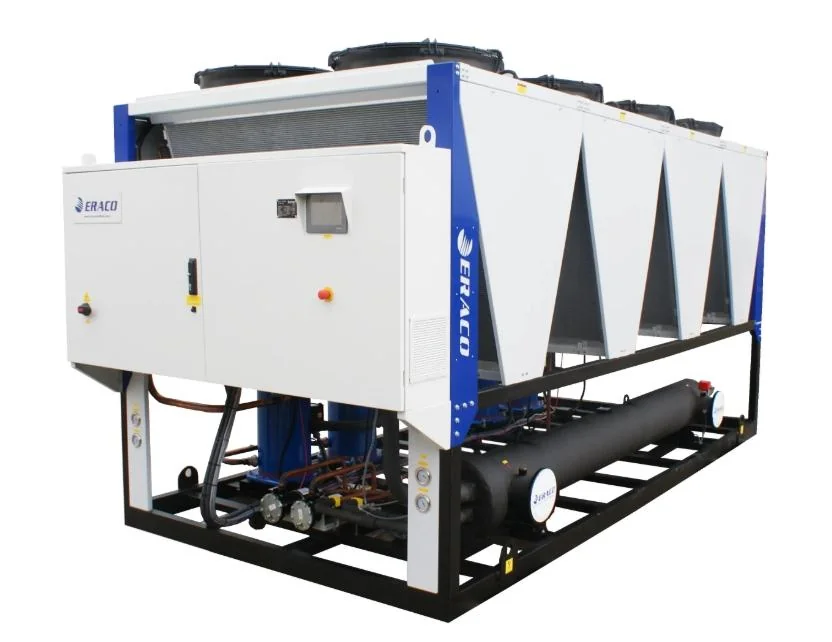
Packaged air-cooled and water-cooled process chillers sized around thermal loads, operating temperatures, and multi-circuit compressor redundancy for continuous cold glycol delivery.
Packaged High-Efficiency Glycol Chilling
ASME BPE · 3-A Sanitary · FAT/SAT Validation
KEYNOH Manufacturing Standards & QA Protocols
Every machine in our capital portfolio is manufactured under rigid quality controls conforming to ASME BPE, 3-A Sanitary Standards, and CE machinery safety directives. Includes complete material traceability certificates (MTC 3.1), surface roughness inspection (<0.8µm Ra), hydrostatic vessel pressure test logs, and comprehensive Factory Acceptance Testing (FAT) before dispatch.
Engineered Specifications
Standard mechanical & process features built into this system.
High-efficiency multi-circuit compressors
Standard factory integration with automated interlocks.
Microprocessor digital staging controls
Standard factory integration with automated interlocks.
Integrated glycol buffer tank & pumps
Standard factory integration with automated interlocks.
Eco-friendly R410A / R134a refrigerant
Standard factory integration with automated interlocks.
Target Product Applications
Complementary Process Systems
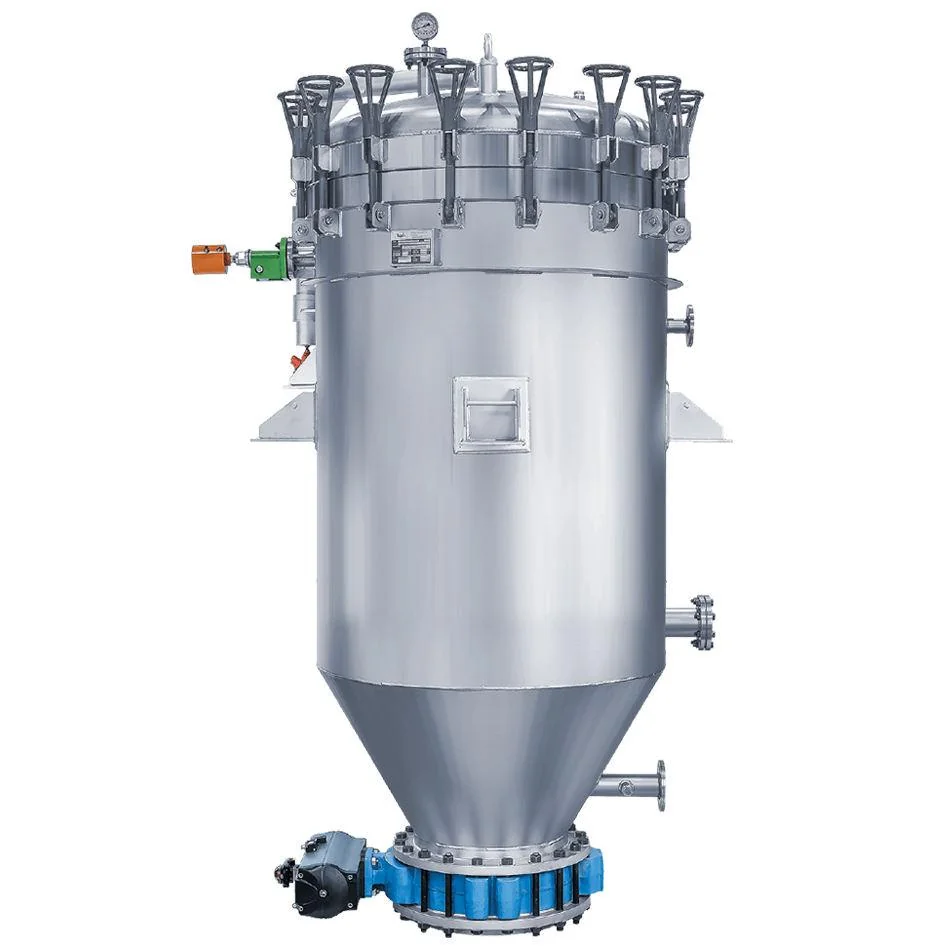
Vertical Pressure Leaf Filter (VPLF)
Enclosed high-capacity filtration for edible oils, fats and process liquids; configurable in food-grade stainless steel with filter-aid dosing, cake drying and automated discharge options.
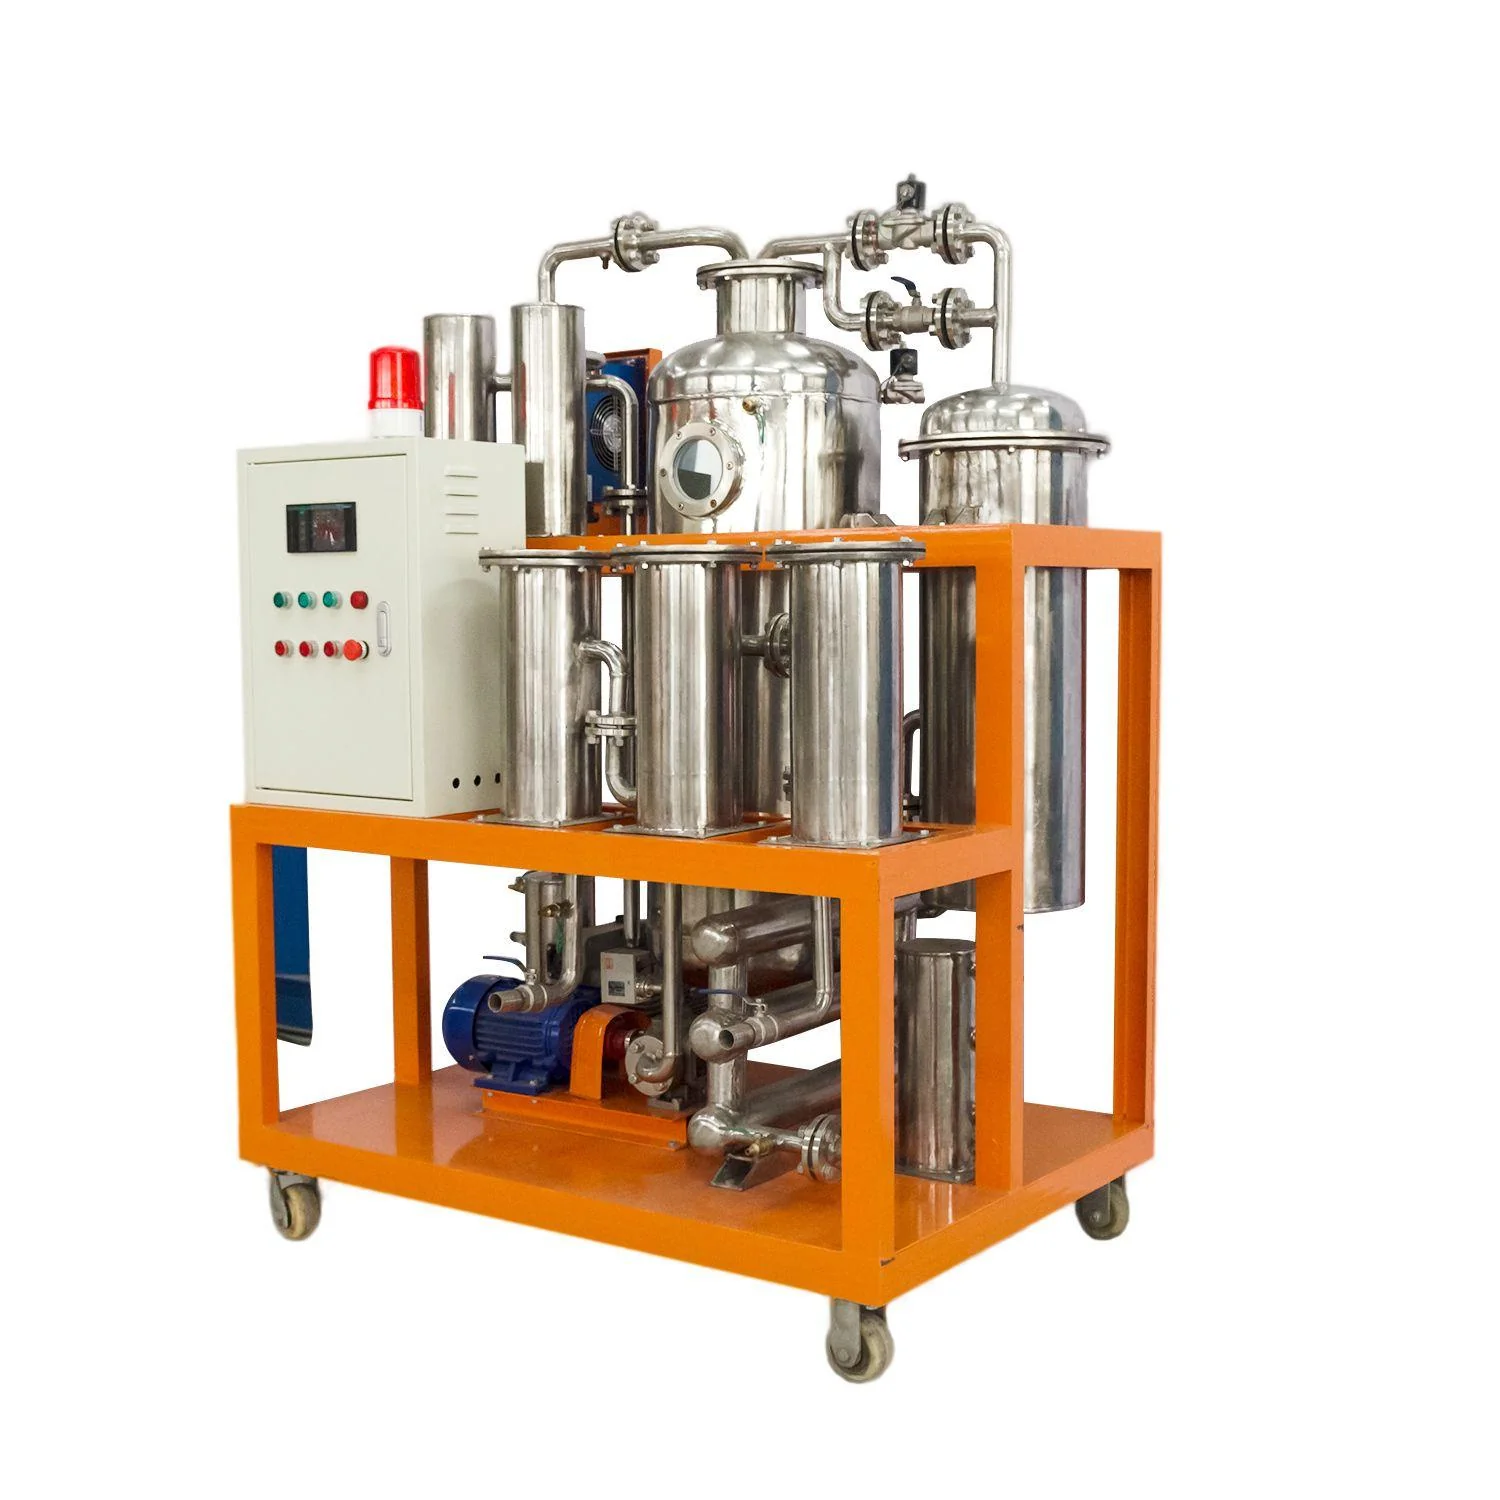
Vacuum Oil Dehydration System
Low-vacuum oil drying and dehydration systems for moisture reduction down to <0.05% while protecting heat-sensitive product aroma and quality characteristics.
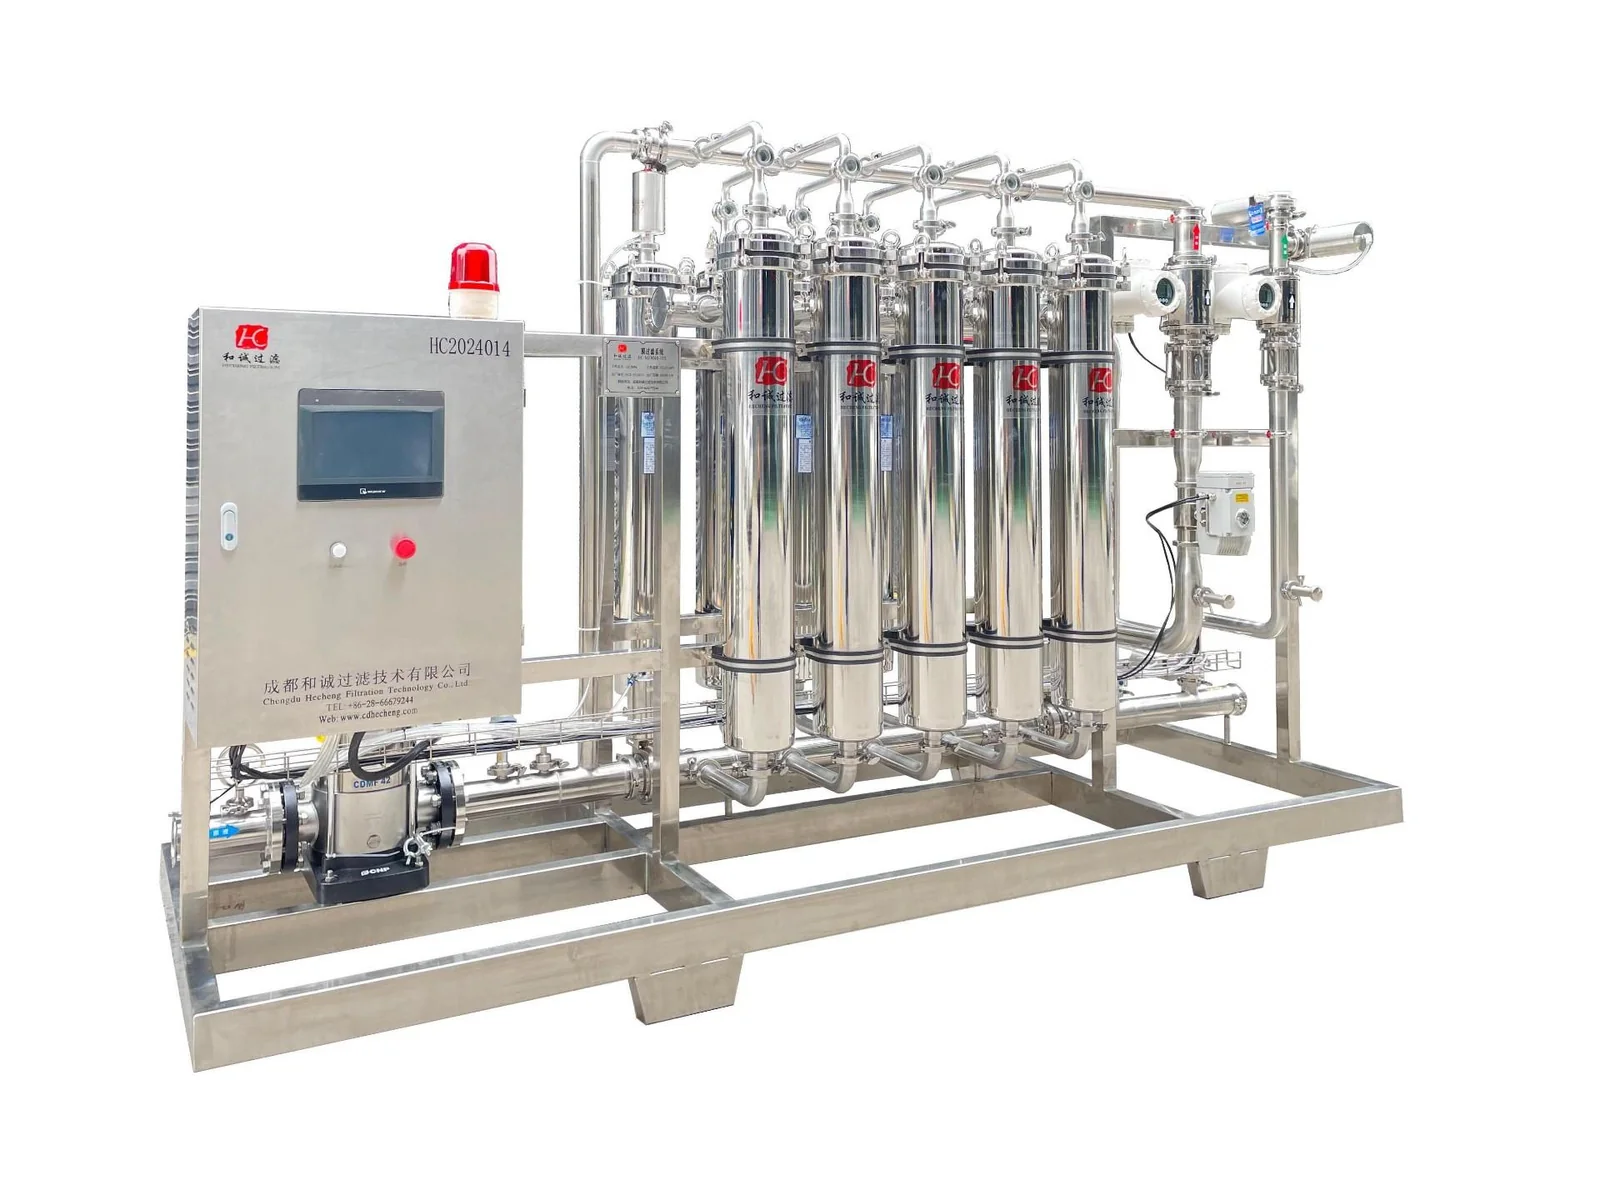
Ultrafiltration System
Hollow-fiber and spiral-wound ultrafiltration units engineered for dairy protein fractionation, juice clarification, plant-based concentration, and final-stage polishing.
Request a Formal Quotation for Industrial Chiller
Connect with our mechanical & automation engineering team for technical datasheets, sizing calculations, utility load schedules, and turnkey installation timelines.